Leave Your Message

How to Source Vitamin A Palmitate Powder in Bulk

Sourcing Vitamin A Palmitate Powder in bulk requires more than comparing prices. Buyers must evaluate identity, potency, stability, documentation, and supplier reliability. A bright quotation can still hide weak testing or inconsistent batches. That matters.

Dr. John N. Hathcock, a respected vitamin safety researcher, has emphasized, “Risk assessment must consider dose, duration, and total exposure.” This principle also guides responsible procurement. A suitable supplier should provide a clear specification sheet, recent certificate of analysis, manufacturing details, and evidence of quality-system controls. Confirm the assay method, vitamin A concentration, carrier ingredients, particle characteristics, and moisture limits. These details affect formulation accuracy and shelf life.

Ask how the powder is protected from oxygen, heat, and light. Vitamin A Palmitate Powder may arrive in sealed foil bags, fiber drums, or nitrogen-flushed containers. Packaging should match the expected storage period and shipping conditions. Request stability data when possible, especially for large-volume orders. Review minimum order quantities, production capacity, lead times, and sample-to-batch consistency. An on-site or remote supplier audit can reveal more than a polished website.

The cheapest offer may not be the lowest total cost. Delays, failed testing, and reformulation can quickly erase savings. Still, supplier claims should not be accepted blindly. Independent verification is sensible. Buyers should also confirm that the product meets the destination market’s applicable food, supplement, cosmetic, or pharmaceutical requirements. A documented comparison table makes decisions clearer and exposes missing information before money changes hands.
How to Source Vitamin A Palmitate Powder in Bulk

Understanding Vitamin A Palmitate Powder and Its Bulk Applications

Vitamin A palmitate powder is a stable, preformed vitamin A ingredient. It is commonly used in dietary supplements, fortified foods, premixes, and animal nutrition. The compound is an ester of retinol and palmitic acid. Its powder form often improves handling, dosing, and dispersion. However, it is not automatically stable. Light, oxygen, heat, and moisture can reduce potency during storage.

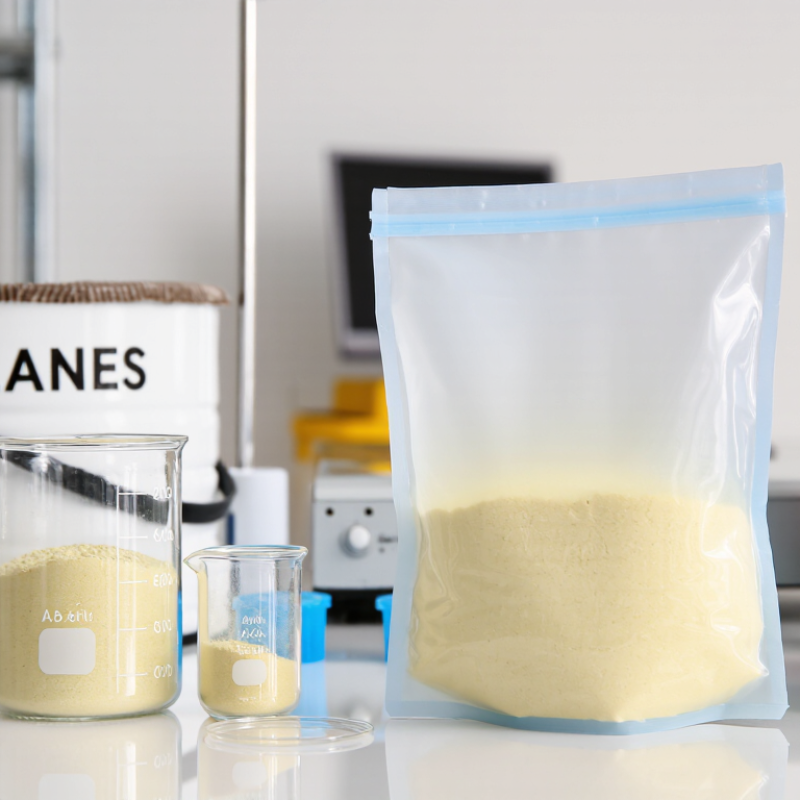
The need remains significant. The World Health Organization reports that vitamin A deficiency affects about 190 million preschool children and 19.1 million pregnant women worldwide. This data supports continued demand for reliable fortification materials. When sourcing in bulk, buyers should review assay strength, carrier composition, particle size, and encapsulation method. A certificate of analysis should confirm identity, potency, microbiological limits, and residual solvents. Packaging also matters. Opaque, sealed containers usually offer better protection than ordinary transparent bags. A low price can become expensive after potency loss.

Tips: Request recent stability data under real shipping conditions. Confirm the unit of measurement, such as IU per gram or micrograms RAE. Check the recommended storage temperature and retest date. Supplier questionnaires should cover traceability and change-control procedures. I would not approve a large order from one laboratory result alone. Independent verification is imperfect, but it can expose costly inconsistencies.
Defining Quality, Purity, and Regulatory Requirements

How to Source Vitamin A Palmitate Powder in Bulk

Defining quality begins with the material’s identity, not its attractive price. Confirm that the powder contains vitamin A palmitate, also called retinyl palmitate, at the stated concentration. Request a recent certificate of analysis from an independent laboratory. Check assay results, appearance, odor, moisture, particle size, and test methods. Small details matter. The carrier system also requires attention because it can affect dispersion, stability, and labeling.

Purity testing should cover heavy metals, microbial limits, residual solvents, and unwanted oxidation products. Ask for batch-specific results rather than a generic specification sheet. Review the safety data sheet, allergen statement, origin records, and packaging description. Opaque, well-sealed containers can help protect this light-sensitive ingredient. A certificate alone is not proof. Compare it with retained samples, production dates, and traceability records when possible.

Regulatory requirements differ by destination, product category, and intended use. Confirm applicable limits for vitamin A, permitted carriers, labeling language, and health claims before placing a bulk order. Suppliers should demonstrate documented quality systems, controlled manufacturing, change notification, and complaint handling. Independent audits can provide useful evidence, although audits are not perfect. I would also verify storage conditions during transport, because heat exposure may reduce potency before arrival. Leave room for review. A rushed purchasing decision can create compliance problems long after delivery.

Identifying Reliable Suppliers and Comparing Product Specifications

Sourcing vitamin A palmitate powder in bulk requires more than comparing quoted prices. A reliable supplier should provide a current certificate of analysis for every production lot. Check the assay, active vitamin A content, appearance, odor, moisture, and particle size. Ask how samples are stored and shipped. Light and heat can reduce potency. Request a small sample before discussing a large contract. Test it with an independent laboratory when the application is sensitive. That extra check costs money. It can prevent an expensive mistake.

Product specifications should match your process, not just your purchasing sheet. Compare concentration, carrier materials, flowability, solubility, and storage conditions. Confirm whether the powder is free-flowing or prone to caking after opening. Review packaging details, such as foil-lined bags, net weight, and tamper evidence. Traceability matters. Each container should connect to a batch number, manufacturing date, and retest or expiry date. Ask for allergen, microbiological, heavy metal, and residual solvent statements when relevant to your quality system. Documentation must be clear and consistent.

Supplier assessment also depends on communication. Can the technical team explain deviations without vague promises? Do they answer questions with records rather than polished language? Check lead times, minimum order quantities, change-notification procedures, and complaint handling. A supplier may offer a perfect specification sheet but lack dependable delivery. In practical purchasing, the cheapest powder is rarely the lowest-risk option. Still, no checklist is perfect. Recheck critical data when the formula, packaging, or destination changes. Small differences can matter.

Evaluating Pricing, Minimum Orders, and Supply Capacity

How to Source Vitamin A Palmitate Powder in Bulk

Bulk sourcing starts with price, but the lowest quotation can hide costly variables. Grand View Research estimated the global vitamin A market at about USD 1.1 billion in 2023, with continued growth expected through 2030. That demand can tighten availability during feed, food, or supplement production cycles. Ask for a price per kilogram at three volumes, such as 25, 100, and 500 kilograms. Confirm assay, particle size, carrier content, packaging, and freight terms. Otherwise, two “identical” quotes may not be comparable.

Minimum order quantities often depend on concentration and packaging. Small trial orders may cost more per kilogram, while larger orders can reduce production and testing costs. They can also create unnecessary inventory. A practical starting point is one validated batch plus a retained sample. Request a certificate of analysis, batch number, manufacturing date, expiry date, and storage conditions. Keep the paperwork complete.

Supply capacity needs closer scrutiny. UN Comtrade classifies vitamin A and certain derivatives under HS 293621, but it does not isolate vitamin A palmitate powder. This limits simple trade comparisons. Ask suppliers for monthly capacity, current lead time, reserve-stock policy, and evidence from recent shipments. FAO and WHO guidance emphasizes controlled vitamin stability, especially exposure to heat, oxygen, and light. My imperfect view: capacity claims deserve doubt until production records and consistent batch results support them. A fast quote proves little.

How to Source Vitamin A Palmitate Powder in Bulk

Evaluating indicative pricing, minimum orders, and monthly supply capacity by supplier scale

Larger purchasing volumes may reduce the indicative price per kilogram, but they usually require higher minimum orders and longer production planning. Actual pricing depends on potency, grade, packaging, testing requirements, delivery terms, and order frequency.

Indicative bulk-planning benchmarks: pricing is shown in USD/kg, minimum order quantity in kg, and supply capacity in metric tons per month. Confirm current specifications and availability directly with qualified suppliers.

Managing Sampling, Testing, Storage, and Bulk Delivery

How to Source Vitamin A Palmitate Powder in Bulk

Reliable bulk sourcing begins with a representative sample. Request material from the actual production batch, not a convenient warehouse sample. Check the certificate of analysis against your agreed specification. Identity, assay, particle appearance, moisture, oxidation markers, and microbiological results deserve attention. A qualified independent laboratory can verify critical results, especially when the purchase volume is large. Keep a sealed retain sample for later comparison.

Protect the powder from light, heat, oxygen, and moisture during storage. Use intact, food-grade containers with suitable inner liners, and record batch numbers at every movement. A cool, dry warehouse helps, but “cool” should be defined by your quality procedure. Follow the supplier’s storage range rather than guessing. Use stock rotation. Simple, but often missed.

Bulk delivery needs more than a shipping date. Confirm pallet configuration, tamper evidence, transport conditions, and document requirements before dispatch. Review the packing list, batch records, test results, and allergen or contaminant statements where relevant. On arrival, inspect damaged cartons, unusual odor, clumping, and label mismatches before release. Sampling every container may be impractical, yet sampling only one container can hide variation. That trade-off should be documented and reviewed. A perfect process rarely exists; controlled improvement matters more.

How to Source Vitamin A Palmitate Powder in Bulk - Managing Sampling, Testing, Storage, and Bulk Delivery

Stage Data Dimension Practical Requirement or Target Verification Method Bulk-Sourcing Consideration
Product Definition Chemical identity Vitamin A palmitate, the palmitic-acid ester of retinol; CAS Registry Number 79-81-2. Supplier specification, identity testing, and certificate of analysis (COA). Confirm that the requested material is powder or beadlet form rather than an oil concentrate or a different vitamin A ester.
Product Definition Potency declaration Specify potency as mass of vitamin A activity per gram or as a defined international-unit concentration. Do not compare offers until the units and assay basis are identical. Review the specification, assay method, conversion basis, and permitted tolerance. A higher numerical value is not automatically a higher-quality product if the unit basis differs.
Prequalification Regulatory and quality documentation Obtain a current specification, COA template, safety data sheet, allergen statement, GMO statement where relevant, and applicable food or pharmaceutical quality documents. Document review before commercial sampling. Requirements depend on the intended use, destination market, and product classification.
Sampling Sample representativeness Request samples from the same production lot or campaign intended for the first bulk shipment whenever possible. Record lot number, manufacturing date, sample weight, packaging condition, and dispatch date. A laboratory sample from a different lot does not fully qualify the production shipment.
Sampling Sample quantity Use enough material for identity, potency, microbiology, physical testing, formulation trials, and a retained reference sample. Agree the quantity and test plan before dispatch; keep a sealed reserve sample. Avoid repeated opening and resealing because oxygen, light, and moisture can reduce stability.
Laboratory Testing Identity and assay Identity should conform to the agreed monograph or validated in-house method; potency should fall within the approved specification. Validated chromatographic testing, commonly HPLC or an equivalent qualified method. Use the same assay basis for supplier COA review and independent confirmation testing.
Laboratory Testing Moisture or loss on drying Set a product-specific limit because powder carriers and beadlet systems can have different moisture profiles. Validated loss-on-drying or water-determination method. Moisture control supports flowability, packaging integrity, and storage stability.
Laboratory Testing Microbiological quality Apply limits appropriate to the intended use; commonly reviewed parameters include total aerobic count, total yeast and mold count, and specified pathogens. Testing by a qualified laboratory using recognized microbiological methods. Microbiological limits must be agreed before purchase because food, feed, and pharmaceutical requirements differ.
Physical Testing Appearance, color, odor, and flow Uniform powder or beadlets with no visible foreign matter, abnormal odor, severe caking, or unexplained discoloration. Visual inspection under controlled conditions; add particle-size or bulk-density testing if required by the formulation. Particle size and density affect blending accuracy, segregation, filling, and dust management.
Contaminant Control Heavy metals and contaminants Limits should comply with the applicable legal and customer specification for the destination market and intended use. Use validated elemental analysis and risk-based contaminant testing. Define testing responsibility, reporting units, and action limits in the purchase agreement.
Packaging Primary-container protection Use sealed, food- or pharmaceutical-contact-compatible packaging with an effective barrier against light, oxygen, and moisture. Review packaging construction, closure system, liner, seal, and tamper evidence. Packaging selection is a major control for oxidation and potency loss during transport and storage.
Storage Temperature and environment Store in a cool, dry, well-ventilated area, protected from direct light. Follow the product-specific label or stability data; many materials specify storage below 25 °C. Monitor temperature and humidity where required; investigate excursions. Do not assume that a general warehouse condition replaces the supplier’s validated storage instruction.
Storage Shelf life and retest date Use only within the stated shelf life or retest period and maintain full lot traceability. Check manufacture date, expiry or retest date, COA, and stock rotation records. Request adequate remaining shelf life at delivery, especially for long-distance shipments or slow-moving inventory.
Bulk Delivery Shipment conditions Keep containers closed, protected from heat, moisture, and light, and secured against crushing or puncture. Review transport records, packaging photographs, seal numbers, and temperature data when required. Use transport packaging and routing consistent with the agreed stability requirements.
Receiving Incoming inspection Verify quantity, lot number, container condition, seals, labels, COA, and visible signs of moisture or damage before release. Quarantine the shipment until quality review and any required confirmatory testing are complete. Document discrepancies immediately with photographs and a formal deviation record.
Release Decision Approval criteria Release only when identity, potency, safety, physical attributes, documentation, packaging, and transport conditions meet the approved requirements. Quality-unit review of the complete batch record and test results. Define rejection, deviation, investigation, and corrective-action procedures before the first purchase order.